توضیحات
| مشخصات فنی | |
|---|---|
| مدل | QLH1000 |
| Loading Capacity | 1,000 kg per batch |
| قدرت | 32.6 kW |
| Cooling System | Integrated forced-air refrigeration |
| Steam Requirement | None — no external steam supply needed |
| Trolleys per Batch | 4 × standard 1030 × 1020 × 1860 mm |
| وزن دستگاه | 4,600 kg |
| Overall Dimensions | 1470 × 4600 × 3480 mm |
| Material | SUS304 stainless steel (food-grade) |
| صدور گواهینامه | م. |
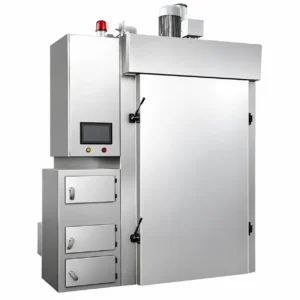
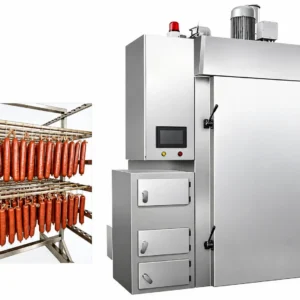
QLH1000 – 1,000 kg High-Volume Smokehouse Machine with Integrated Forced Cooling
The QLH1000 is the largest model in the QLH forced-cooling smokehouse series, designed for high-volume, HACCP-compliant cook-chill production at industrial scale. Processing 1,000 kg per batch across four standard trolleys in a 1470 × 4600 × 3480 mm chamber, the QLH1000 delivers the entire smoking, cooking, and rapid chilling cycle within a single self-contained system — no external steam supply, no separate blast-chilling room, no product transfer between thermal environments. For large-scale ready-to-eat meat producers, poultry integrators, and co-pack facilities operating multiple production shifts, the QLH1000 consolidates two separate process steps into one unit, reducing floor footprint, utility complexity, and product-handling labor.
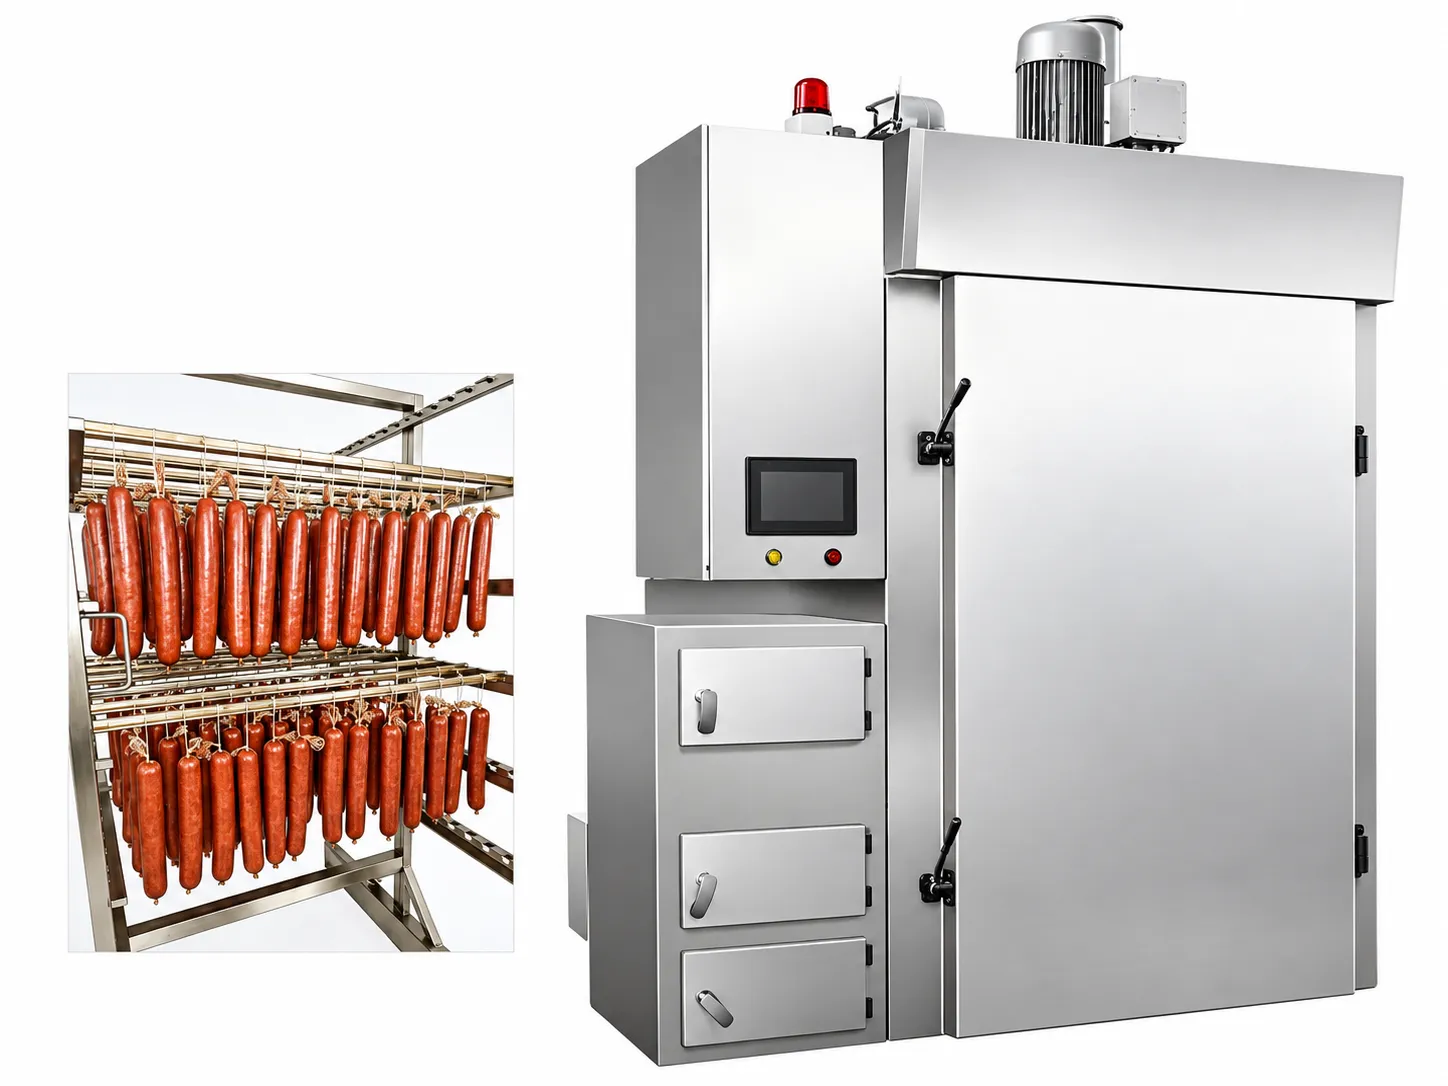
QLH1000 – 1,000 kg four-trolley forced-cooling industrial smokehouse
High-Volume Cook-Chill Engineering
Managing a uniform process environment across a 4,600 mm long chamber containing 1,000 kg of product is the central engineering challenge the QLH1000 addresses. The quad-motor fan array delivers calibrated forced-air circulation from end to end of the chamber, maintaining ±2°C temperature uniformity across all four trolley positions during the cooking phase. The same fan system reverses to cooling mode when the refrigerant circuit activates, drawing chamber air through the full-length heat exchanger mounted above the chamber ceiling. Cooling airflow is distributed evenly across all four trolley bays through the same duct manifold used for heating and smoking, ensuring that temperature reduction is not faster at trolley position 1 than at position 4.
This end-to-end thermal uniformity is particularly important in high-volume cook-chill production because HACCP compliance requires that all product in the batch — not just the front trolley — achieves both the pasteurization minimum and the chilling endpoint within the specified time limits. The QLH1000 achieves this through distributed process management, not by running longer cycles that reduce throughput.
All-Electric Operation – No Steam Infrastructure Required
Like the QLH500, the QLH1000 requires only a 380 V, 3-phase, 50/60 Hz electrical connection. The elimination of the steam supply requirement has compounded impact at 1,000 kg batch scale: a QZX1000 installation requires a boiler capable of supplying steam at 0.3–0.6 MPa for a 1,000 kg load, plus all associated pipework, pressure-reducing stations, and water-treatment systems. The QLH1000 avoids this entire infrastructure layer, which for new-build facilities can represent a substantial portion of total site capex.
The 32.6 kW total electrical draw of the QLH1000 covers all fans, the heating system, the refrigeration compressor, controls, and the smoke generator. There are no separately metered utility costs for steam. For multi-shift operations running three or more production cycles per day, the reduction in boiler fuel cost and water treatment expense contributes measurably to per-kilogram production cost over the machine’s operating life.
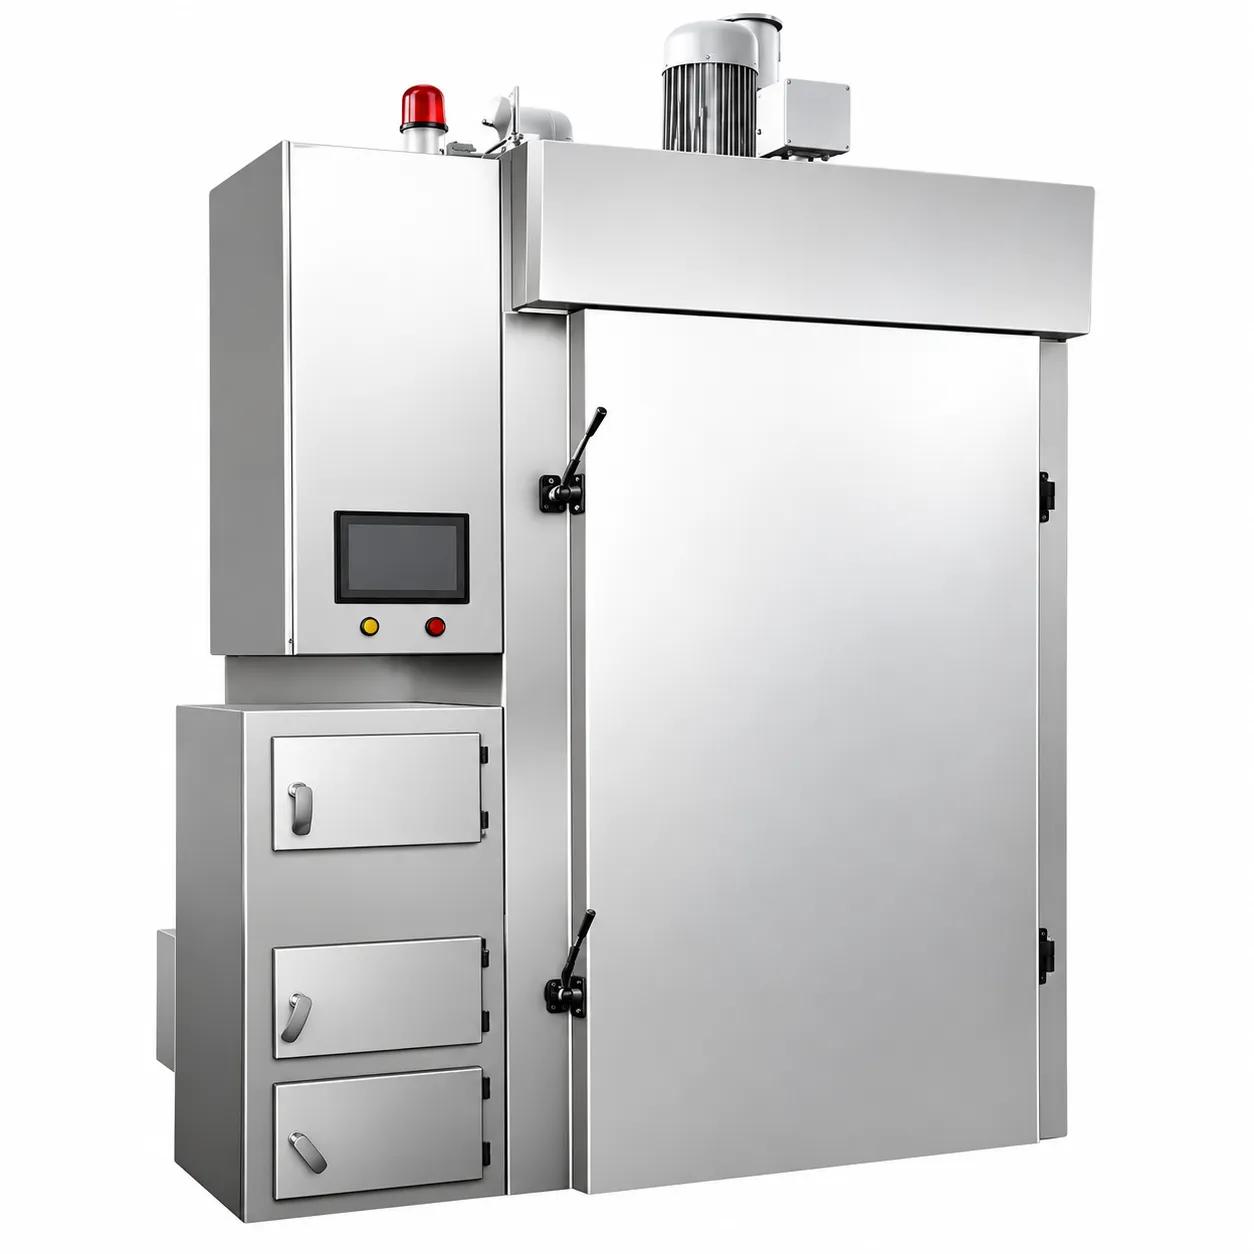
QLH1000 chamber interior showing smoke-distribution baffles and cooling system
HACCP Compliance at Scale
The QLH1000 is designed from the ground up for HACCP-regulated, multi-shift RTE production. The HACCP hold-step interlock prevents the cooking phase from advancing to cooling if the core-temperature probe does not confirm pasteurization temperature within the programmed cook time. The cooling phase runs until the target endpoint temperature is confirmed in all monitored zones, not just the closest probe position. Both confirmations are logged as HACCP critical control point records in the batch file.
Process data logging covers chamber temperature at six measurement points, air velocity, smoke density, refrigerant-circuit suction and discharge pressures, and product core temperature at 10-second intervals throughout every batch. The rolling 90-day on-board archive and USB export function provide the documentary evidence required for BRC Global Standard, IFS Food, FSSC 22000, USDA FSIS, and retailer-specific audit programs. PIN-secured operator log-in associates each batch record with the shift and operator responsible, completing the chain of custody from raw product loading to cooled product release.
Recipe version control: the QLH1000 PLC retains all previous versions of each recipe with timestamps when modifications are saved. This satisfies the change-management documentation requirement of formal food-safety quality systems and prevents accidental overwrite of validated production recipes in multi-shift environments where multiple operators access the HMI.
Daily Throughput & Production Economics
At 1,000 kg per batch and two batches per 8-hour shift, the QLH1000 delivers 2,000 kg of finished cook-chill smoked product per shift. At three shifts per day, daily output reaches 6,000 kg. For comparison, the QLH500 delivers 3,000 kg per day at the same shift pattern. The cost-per-kilogram economics of the QLH1000 improve substantially at this output volume: fixed costs (amortization, space, labor) spread across twice the batch size of the QLH500, while variable costs (electricity, smoke fuel) scale approximately linearly. For facilities with consistent demand above 3,000 kg per day, the QLH1000 is typically the more cost-efficient specification.
- Large-scale RTE cook-chill operations: 6,000 kg/day finished product at 3-shift operation
- Poultry integrators: high-volume whole-bird and portion smoking with HACCP compliance
- Export co-packers: consistent, auditable multi-SKU programs for retail-branded products
- Multi-site hub kitchens: centralized cooked-product production for distribution networks
- Vertically integrated processors: finishing capacity matched to upstream brine-injection lines
Smoke Delivery & Atmosphere Control at 1,000 kg Scale
Maintaining consistent smoke density across a 4,600 mm long chamber with 1,000 kg of product requires active closed-loop management. The QLH1000 smoke generator feeds conditioned hardwood smoke through the full-length distribution manifold, delivering simultaneous smoke exposure to all four trolley bays. The optical smoke-density sensor in the exhaust duct monitors actual chamber concentration and feeds back to the PLC, which modulates generator output to maintain the recipe target. This prevents the early-cycle over-concentration that occurs in large chambers where the smoke-to-volume ratio is difficult to manage without feedback control, and it ensures that the surface phenol and carbonyl deposition — which determines both flavor intensity and surface color — is uniform from trolley position 1 to position 4.
The forced-air distribution system in the QLH1000 delivers smoke at higher velocity than a passive-draft smokehouse, reducing smoke-phase time and improving penetration uniformity across densely loaded trolleys. For high-volume product categories such as whole-bird poultry, bone-in ham, or large coarse-ground sausage, this combination of velocity and density control produces consistent surface color development that meets retail product-appearance specifications without batch-to-batch color-sorting. The same air-circulation system that delivers smoke also manages the drying and color-development phases, so the entire pre-cooling process cycle is handled by one integrated air-management architecture rather than separate mechanisms for each phase.
سوالات متداول
How does the QLH1000 compare to the QLH500?
The QLH1000 processes 1,000 kg per batch (four trolleys) versus 500 kg (two trolleys) in the QLH500. Chamber length extends to 4,600 mm versus 2,600 mm. Power draw is 32.6 kW versus 16.6 kW. Process technology, HACCP controls, and trolley standard are identical. The QLH1000 offers lower cost-per-kilogram at consistent high-volume production due to fixed-cost spreading across the larger batch size.
What ceiling height does the QLH1000 require?
The QLH1000 stands 3,480 mm tall. A minimum ceiling clearance of 3,800 mm is recommended for service access to the refrigeration unit above the chamber. Standard industrial production ceilings of 4 m or above are typically sufficient.
Is a pass-through configuration available for the QLH1000?
Yes. A double-door pass-through option is available for the QLH1000 for use in continuous-flow production lines maintaining physical separation between raw and cooked product areas. Specify at the inquiry stage so it is captured in the production drawing.
What refrigerant does the QLH1000 use?
Standard configuration uses R404A or the lower-GWP R452A. The specification is confirmed at order stage based on the buyer’s local environmental regulations. The refrigeration unit is factory pre-charged and pre-commissioned; no on-site refrigerant work is required during installation.
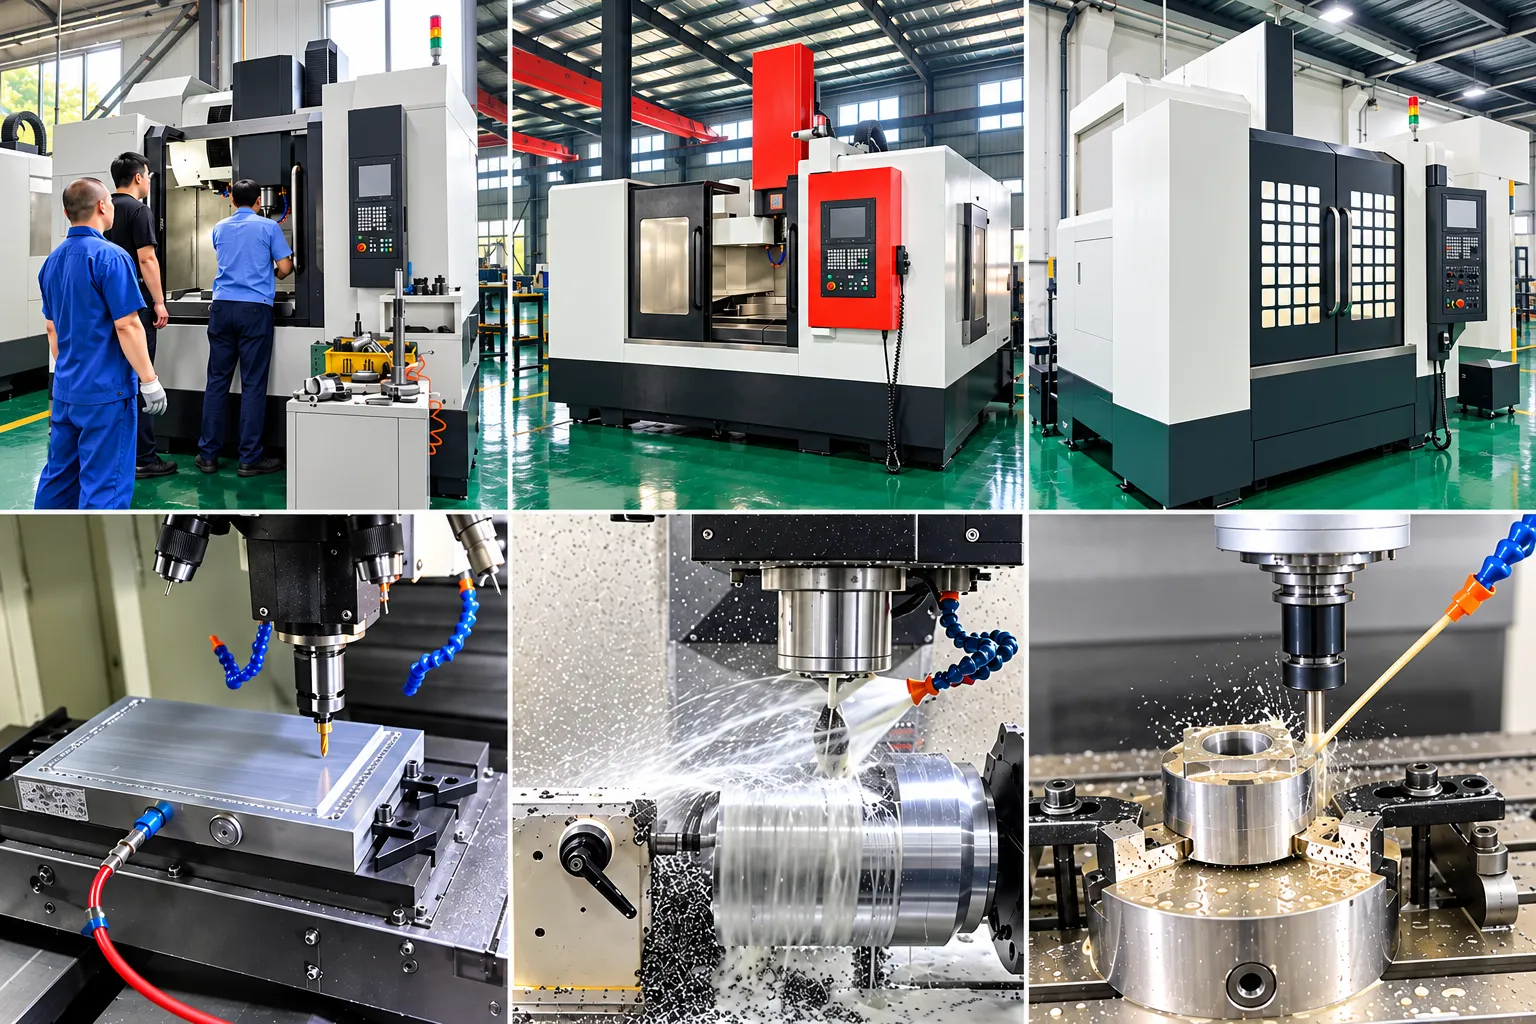
QLH1000 pre-shipment testing – Hebei Province factory
درباره سازنده
Backed by 25+ years of manufacturing experience, our Hebei Province plant delivers smokehouse ovens built to strict food-grade stainless-steel and CE safety standards. From a 5,000 m² campus staffed by over 100 professionals, we handle every stage in-house: steel fabrication, control-panel assembly, pre-shipment functional testing, and export documentation. Our global customer base includes independent meat processors, hotel kitchen operators, and large-scale co-packing facilities. Email us at [email protected].
Shipping & After-Sales
Our logistics team handles all export formalities including customs documentation, insurance cover to the buyer’s destination port, and phytosanitary certificates where required. Standard lead time is 30–45 working days. Equipment is pre-tested for 8 hours before dispatch. Post-delivery technical support is provided by email, WhatsApp, and video call. Consumable items — gaskets, heating elements, smoke-generator components — are stocked for rapid dispatch.
- Full export documentation and logistics management
- 8-hour pre-dispatch test with parameter report
- Post-delivery support: email, WhatsApp, video call
- Consumables stocked for rapid dispatch
- Lead time: 30–45 working days from deposit
سفارش و لجستیک
Each order is supported end-to-end: engineering consultation, production scheduling, pre-shipment testing, export documentation, and post-delivery technical support. Lead time: 30–45 working days. Payment: T/T 30% with order, 70% before shipment; L/C accepted. FOB Tianjin standard; CIF, DAP, and DDP available. Commissioning support via video call included within 30 days of delivery.
Start Your Order
Provide your capacity, food type, and port of destination for a detailed quotation and delivery timeline.
محصولات و صفحات مرتبط