விளக்கம்
| தொழில்நுட்ப விவரக்குறிப்புகள் | |
|---|---|
| மாதிரி | QZX500 |
| Loading Capacity | 500 kg per batch |
| சக்தி | 16.6 கிலோவாட் |
| High-Pressure Steam | 0.3–0.6 MPa |
| Low-Pressure Steam | ≤0.1 MPa |
| Max Temp (Smoke) | <85°C |
| Max Temp (Cooking) | <100°C |
| Trolleys per Batch | 2 × standard 1030 × 1020 × 1860 mm |
| இயந்திர எடை | 2,500 kg |
| Overall Dimensions | 1475 × 2235 × 2500 mm |
| Material | SUS304 stainless steel (food-grade) |
| கிரிக்கெட் | சிஇ |
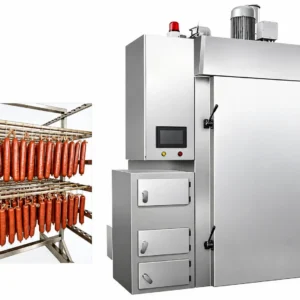
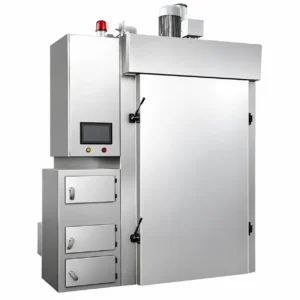
QZX500 – 500 kg Industrial Smokehouse Cooking Machine
The QZX500 is a 500 kg per batch industrial smokehouse cooking machine designed for regional meat processors, co-packing operations, and vertically integrated food producers seeking to scale up from single-trolley pilot capacity to genuine production volume. Accommodating two standard trolleys side by side in its 1475 × 2235 × 2500 mm chamber, the QZX500 doubles throughput while maintaining the identical steam-injection technology and PLC control architecture used in the smaller QZX250. At 16.6 kW and 2,500 kg net weight, it represents the optimum balance of floor-space efficiency and output for facilities processing up to 2,000 kg of finished product per eight-hour shift.
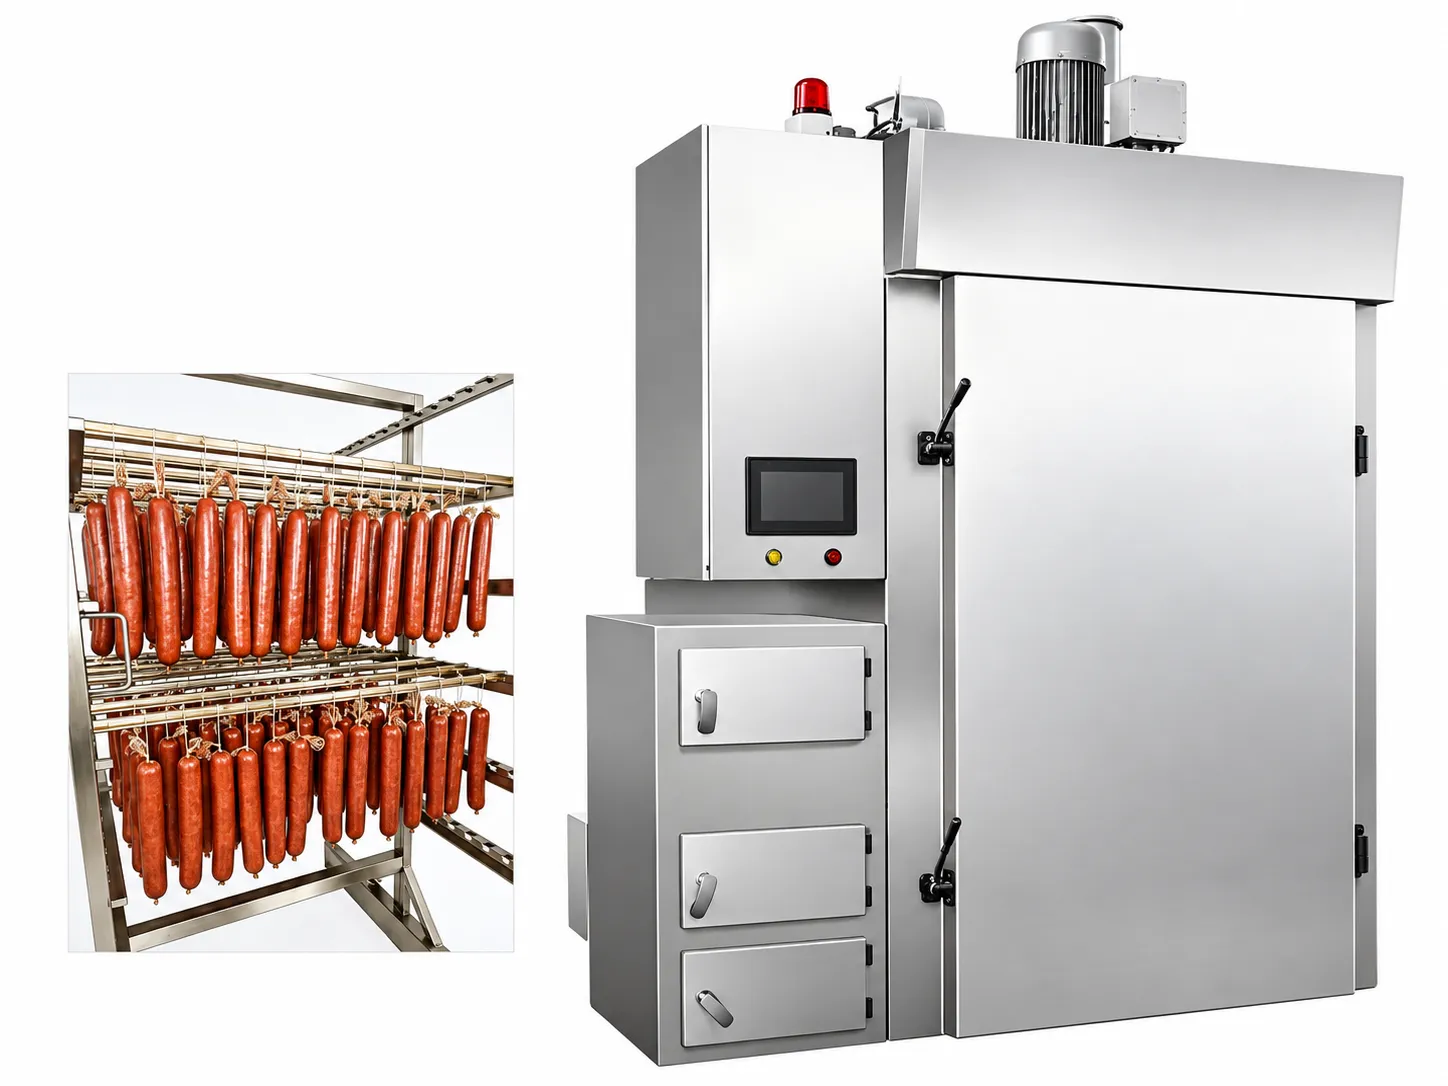
QZX500 – 500 kg two-trolley steam-injection smokehouse
Two-Trolley Chamber Architecture
The defining feature of the QZX500 is its twin-trolley loading configuration. Two standard 1030 × 1020 × 1860 mm trolleys roll in side by side through the single front door. Because the trolley dimensions are identical to those used in the QZX250 and QZX1000, existing trolleys, hanging bars, and mesh-tray sets are fully interchangeable across a mixed-capacity smokehouse fleet. Facilities that currently operate a QZX250 can add the QZX500 without purchasing new trolley hardware or retraining loading staff.
Horizontal air circulation is provided by dual top-mounted fan motors that maintain measured temperature uniformity of ±2°C across the complete chamber volume. Airflow velocity is independently programmable per recipe phase: higher velocities during the pre-drying phase accelerate surface moisture removal; lower velocities during smoke application minimize turbulence and improve phenol compound deposition. This programmable air-management system is common to all QZX models and carries over the same operator interface from the QZX250, simplifying staff cross-training.
Dual-Circuit Steam Injection & Moisture Control
Like all QZX series machines, the QZX500 uses a dual steam-injection architecture. The high-pressure circuit (0.3–0.6 MPa) delivers pulsed steam to rapidly elevate chamber humidity at the start of cooking and during moisture-injection phases, driving moisture into the product mass and promoting even heat penetration throughout a densely loaded 500 kg batch. The low-pressure circuit (≤0.1 MPa) sustains a precise ambient-humidity environment during the sustained cooking stage, suppressing evaporative loss and delivering the product weight-retention figures that QC targets require.
Temperature management covers the full range from ambient to the defined cooking ceiling of below 100°C. The smoke-application phases operate below 85°C — the temperature window that maximizes the deposition of the flavor-active phenols and carbonyls found in hardwood smoke. Phase transitions between pre-drying, smoking, cooking, and color-fixation are fully automated by the on-board PLC; operators load the trolleys, select the recipe, and the machine advances through the cycle without manual intervention.
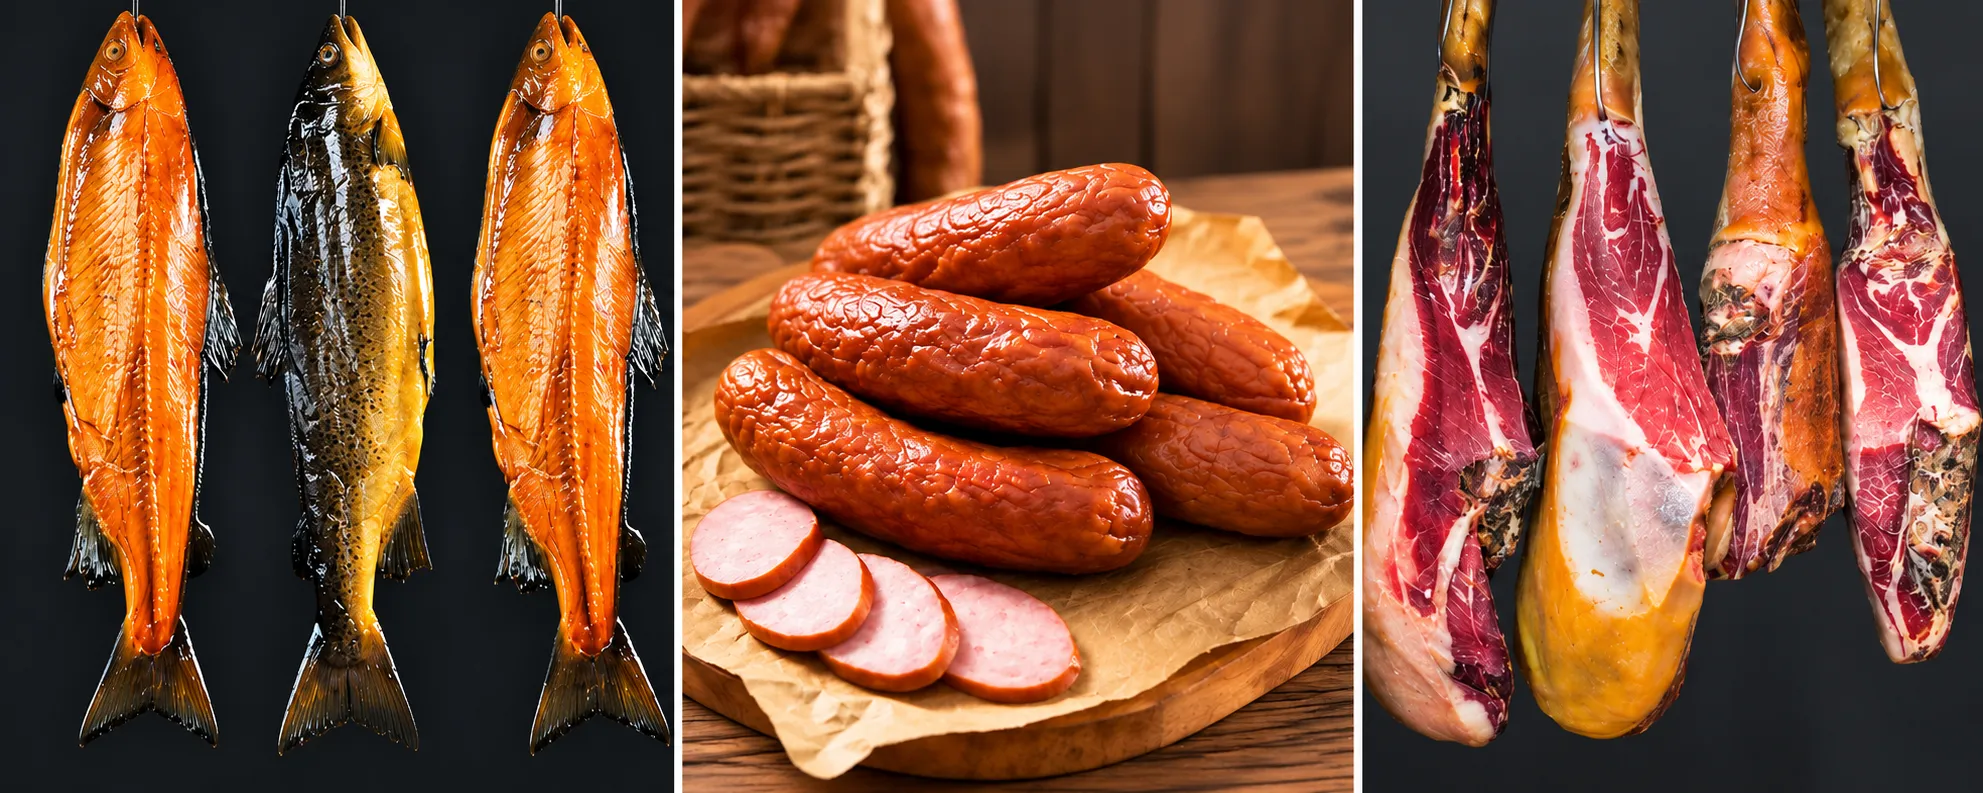
Smoked hams, sausages, and poultry produced in the QZX500
PLC Recipe Management & Traceability
The QZX500 uses a Siemens or Mitsubishi PLC (specified at order) with a 7-inch color touch-screen HMI. Up to 99 independent recipe programs are stored on-board. Each program defines phase-by-phase settings for chamber temperature, high-pressure steam interval and duration, low-pressure steam level, smoke density target, air-circulation speed, and phase hold time. Pre-loaded templates for common product types are editable on the production floor HMI without factory involvement.
Process data — temperature at four measurement points, both steam-circuit pressures, air velocity, and smoke density — is logged at 10-second intervals throughout every batch. Logs are stored in a rolling 90-day archive and are exportable via USB for HACCP, BRC, IFS, or FSSC 22000 documentation. Batch records include operator PIN log-in, recipe name and version, and any parameter deviation alarms, providing a complete chain-of-custody audit trail for every production run.
Space-efficiency note: the QZX500 processes twice the QZX250 batch size in a floor footprint only 1,095 mm longer (1475 × 2235 mm vs. 1475 × 1140 mm). For facilities with limited floor area, this linear extension minimizes the impact on workflow corridors and service access compared to installing two QZX250 units.
Applications & Throughput Planning
The QZX500 is the first choice for processors targeting the following output profiles:
- Regional deli and charcuterie producers: 1,000–2,000 kg finished product per shift
- Co-packing and contract manufacturing: consistent, auditable multi-batch production
- Export-oriented smokehouse operations: scalable volume for ocean-container packing
- Hotel and institutional central kitchens: high-variety, multi-product weekly schedules
- Poultry integrators adding a value-added smoked-bird product line
At two batches per eight-hour shift, the QZX500 delivers 1,000 kg/shift of finished product. At three shifts per day, daily output reaches 3,000 kg — sufficient to supply a significant retail or food-service distribution network from a single unit. When demand grows further, the QZX1000 offers four-trolley capacity with the identical process performance, using the same trolleys and the same operator training.
Electrical & Utility Requirements
The QZX500 requires a 380 V, 3-phase, 50/60 Hz supply at 16.6 kW rated draw. Factory-installed main isolator and earth-leakage circuit breaker are standard. The IP65-rated control panel is sealed against wash-down water ingress. An external steam supply is required: connect the high-pressure circuit (0.3–0.6 MPa) and low-pressure circuit (≤0.1 MPa) inlets to the facility boiler or a dedicated steam generator. No gas or oil burner is integrated into the machine; the 16.6 kW electrical load covers all fans, controls, and the smoke generator only.
Wood Fuel, Smoke Chemistry & Flavor Development
The smoke flavor and color characteristics of the finished product depend on the wood species, chip size, and smoke-generator temperature used in the QZX500. Beech and hickory produce a bold, full smoke profile suited to whole-muscle hams and beef cuts. Cherry, apple, and alder yield a milder, slightly sweet smoke character preferred for poultry, fish, and artisan charcuterie. The smoke generator pyrolyzes wood material at a controlled temperature without open combustion, producing a cool, predominantly phenolic smoke that deposits color-active carbonyls on the product surface during the dedicated smoke phase at below 85°C. This temperature-controlled generation method minimizes polycyclic aromatic hydrocarbon levels and gives operators a reproducible flavor baseline that does not vary between batches, between operators, or over time as the machine ages.
Smoke density in the QZX500 chamber is managed by a closed-loop optical sensor and PLC feedback system: the sensor measures actual smoke concentration in the exhaust stream and the PLC modulates smoke-generator output to maintain the target density set in the active recipe. This automation removes the manual judgment that causes batch-to-batch color variation in manually controlled smokehouse systems, and it ensures that the two trolleys in the QZX500 chamber receive identical smoke exposure regardless of their position relative to the smoke inlet. Over a production shift of multiple batches, the system maintains color and flavor consistency that satisfies the uniformity specifications of retail buyers and food-service procurement programs.
அடிக்கடி கேட்கப்படும் கேள்விகள்
How does the QZX500 differ from the QZX250?
The QZX500 holds two trolleys (500 kg) versus one trolley (250 kg) in the QZX250, in a chamber 1,095 mm longer. Power draw doubles to 16.6 kW. All process technology — steam circuits, PLC system, temperature range, and trolley standard — is identical. Operators trained on the QZX250 require no additional training to operate the QZX500.
What steam supply specification does the QZX500 need?
The QZX500 requires a high-pressure steam supply at 0.3–0.6 MPa and a low-pressure supply at ≤0.1 MPa. Both circuits require separate control valves and pressure-reducing stations. Share your boiler capacity and pipe-run details and our engineers will specify the connection hardware.
Can the QZX500 handle a pass-through workflow?
A double-door pass-through option is available, allowing raw product to enter from one side and cooked product to exit on the opposite side, maintaining physical separation in HACCP-zoned facilities. Specify this requirement at the inquiry stage.
What is the temperature uniformity inside a fully loaded QZX500?
Temperature uniformity of ±2°C across the full chamber volume is verified during the 8-hour pre-shipment test on every unit. This is measured at multiple locations across both loaded trolley positions simultaneously.
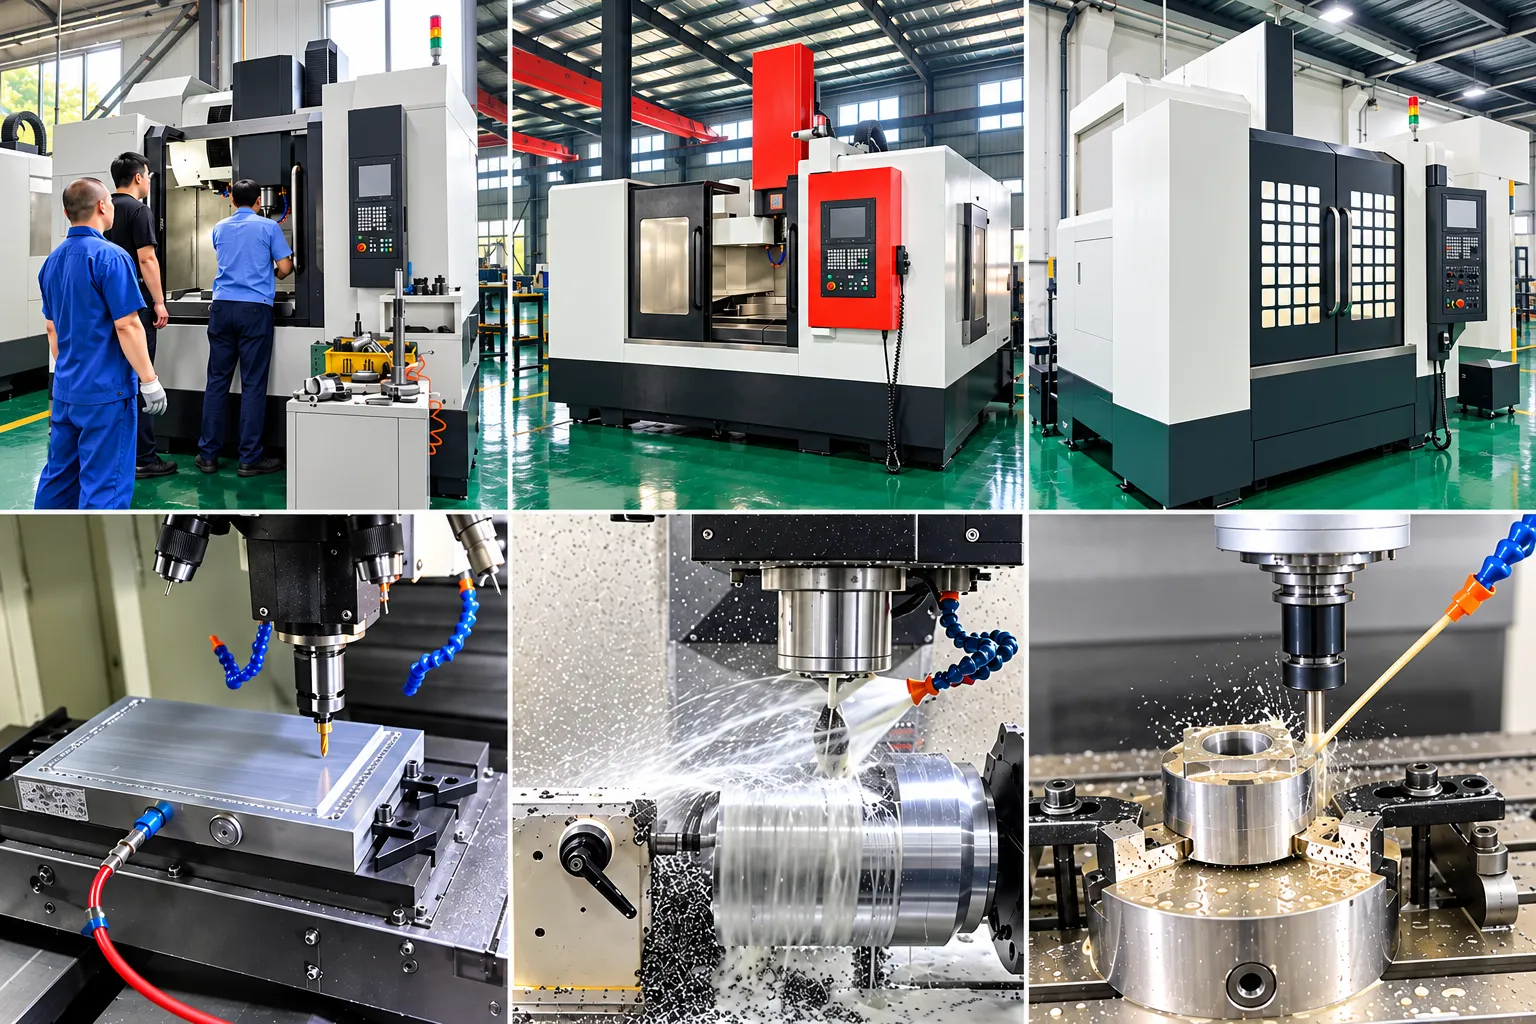
QZX500 production and pre-shipment testing – Hebei Province factory
உற்பத்தியாளரைப் பற்றி
Founded in 1999, our Hebei Province campus spans 5,000 m² and employs over 100 engineers, machinists, and after-sales technicians. We serve the full cooked-meat and sausage processing workflow — from brine injection and tumbling through smoking, filling, and clipping. Machines are built to food-grade SUS304 stainless steel standards with IP65-rated control panels and CE-compliant electrical systems. Email [email protected] for a quotation, technical datasheet, or factory audit schedule.
Shipping & After-Sales
Each smokehouse oven undergoes a full 8-hour run test before crating. Shipments leave FOB Tianjin Port within 30–45 working days of deposit receipt. Documentation package includes commercial invoice, packing list, CE certificate, and a bilingual operation manual. We maintain a spare-parts inventory for all current models; standard components ship within 3 business days of order. The one-year warranty covers all non-consumable mechanical and electrical components.
- Lead time: 30–45 working days post-deposit
- Shipment: FOB Tianjin (CIF / EXW on request)
- Documentation: invoice, packing list, CE certificate, manual
- Warranty: 1 year on mechanical and electrical components
- Spare parts stocked, dispatched within 3 business days
ஆர்டர் மற்றும் தளவாடங்கள்
Standard production cycle: 30–45 working days. Shipping: FOB Tianjin (CIF, EXW, DAP on request). Payment: T/T 30% advance deposit, 70% prior to loading; L/C at sight accepted. Each order is assigned a dedicated project manager. New buyers may place sample orders without a fixed piece-count minimum.
Get Pricing & Availability
Share your capacity requirement and delivery port — our team responds within one business day.
தொடர்புடைய தயாரிப்புகள் மற்றும் பக்கங்கள்