تفصیل
| تکنیکی وضاحتیں | |
|---|---|
| ماڈل | QLH500 |
| Loading Capacity | 500 kg per batch |
| طاقت | 16.6 کلو واٹ |
| Cooling System | Integrated forced-air refrigeration |
| Steam Requirement | None — no external steam supply needed |
| Trolleys per Batch | 2 × standard 1030 × 1020 × 1860 mm |
| مشین کا وزن | 2,800 kg |
| Overall Dimensions | 1470 × 2600 × 3480 mm |
| Material | SUS304 stainless steel (food-grade) |
| سرٹیفیکیشن | عیسوی |
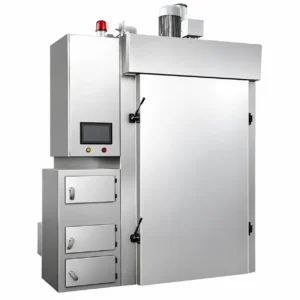
QLH500 – 500 kg Smokehouse Machine with Integrated Forced Cooling
The QLH500 is a 500 kg per batch smokehouse machine that integrates smoking, cooking, and rapid post-cook forced-air chilling within a single, self-contained chamber — and requires no external steam supply. Unlike steam-injection smokehouse systems, the QLH500 achieves its cooking and moisture-management objectives through precisely controlled high-velocity forced air, then switches to refrigerant-cooled airflow for HACCP-compliant rapid chilling without moving the product between chambers. The QLH500 is specifically designed for facilities that either lack central boiler infrastructure, or where integrating post-cook chilling into the smokehouse cycle reduces capital investment and floor footprint compared to a separate steam-injection smokehouse plus external blast chiller.
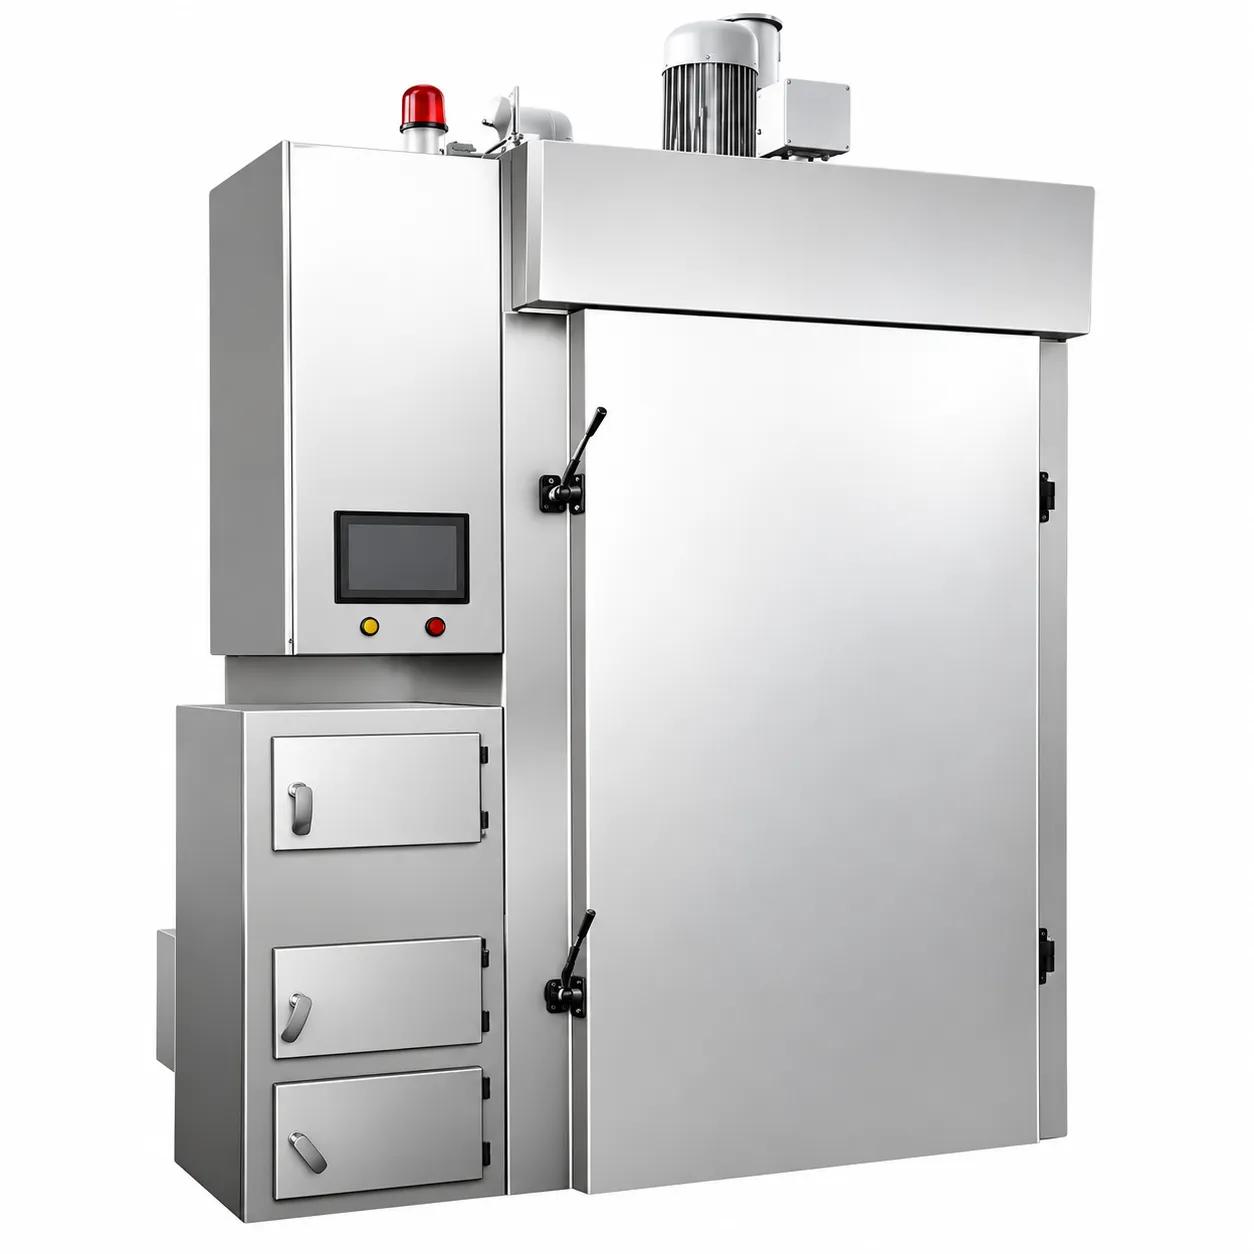
QLH500 – 500 kg forced-air cooling smokehouse, no steam required
No Steam Required – All-Electric Forced-Air Process
The most operationally significant feature of the QLH500 is the elimination of the steam supply requirement. The QZX steam-injection series requires connection to a facility boiler or standalone steam generator at 0.3–0.6 MPa and ≤0.1 MPa. The QLH500 connects only to a standard 380 V, 3-phase, 50/60 Hz electrical supply. This single-utility requirement reduces installation cost and complexity, and makes the QLH500 deployable in a wide range of facility types that would otherwise require significant boiler infrastructure investment before a steam-injection smokehouse could be commissioned.
All heating, smoking, moisture management, and chilling functions are handled by the integrated all-electric forced-air system. The variable-speed fan array at the chamber top drives heated, smoke-laden air across the product load during the cooking and smoking phases, then transitions to cooling mode by activating the refrigerant circuit and routing chamber air through the internal heat exchanger. Chamber temperature drops continuously without opening the door or handling the product — a single-environment cook-and-chill cycle that reduces contamination risk during the critical post-cook temperature window.
Integrated HACCP Rapid Chilling
The QLH500 is designed to meet the industry-standard HACCP requirement of reducing core product temperature from 72°C to below 10°C within 90 minutes following cooking. This requirement, mandated under USDA FSIS guidelines, EU Regulation (EC) 853/2004, and most national food-safety authority frameworks, applies to all ready-to-eat cooked meat products. Meeting it without a dedicated blast-chiller requires the high air-velocity and heat-exchanger capacity that the QLH500 integrates as standard.
The PLC monitors core product temperature via an inserted probe and holds the cooling phase until the required endpoint is confirmed. A HACCP hold-step interlock prevents the system from advancing out of the cooking phase if the pasteurization temperature is not confirmed within the programmed cook time — a safety feature that eliminates the risk of under-processed product entering the cooling stage. Both the cooking-phase confirmation and the cooling-phase endpoint are recorded in the batch log, providing a complete, auditable temperature-control record for every production run.
Capital cost advantage: the QLH500 eliminates the need for a separate blast-chilling room and chiller unit alongside the smokehouse investment. A standalone blast chiller sized for 500 kg typically costs as much as a mid-range smokehouse unit and occupies 5–10 m² of floor space. Consolidating the chilling function into the smokehouse chamber reduces both capex and total floor-space requirement for new-build facilities.
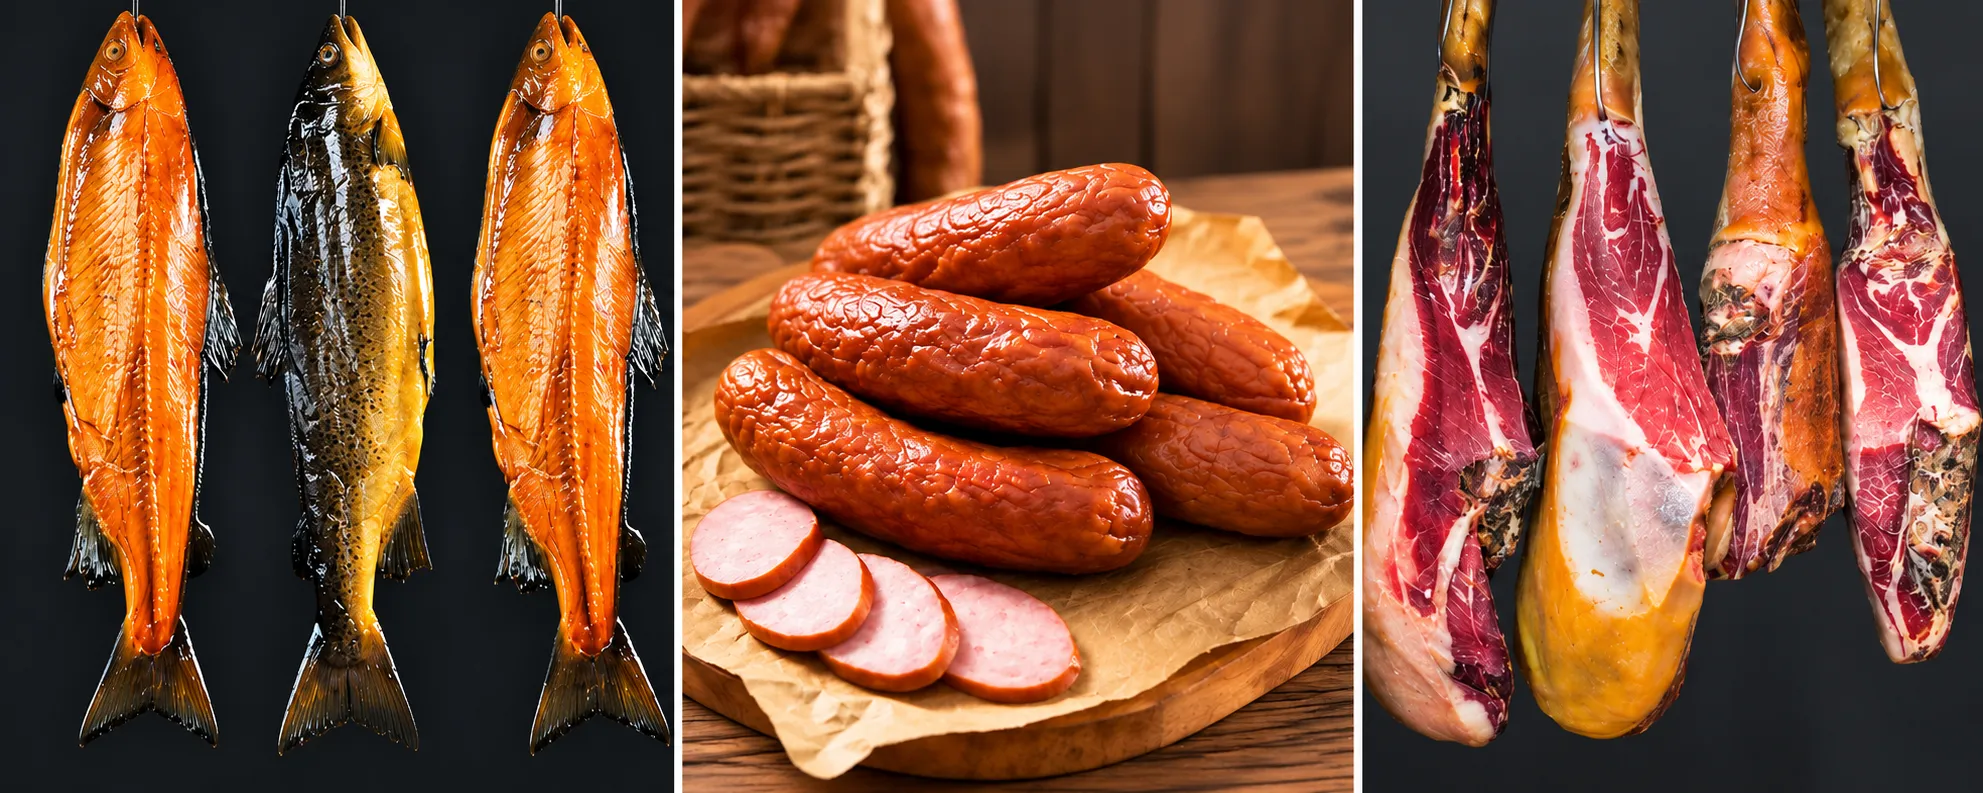
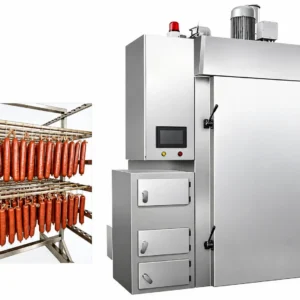
RTE smoked and chilled products from the QLH500
Applications & Facility Profiles
The QLH500 is the preferred smokehouse specification for:
- Ready-to-eat cook-chill production lines where HACCP rapid chilling is mandatory
- New-build facilities designed without central boiler infrastructure
- Remote or modular production units with limited utility connections
- Poultry smoking lines where consistent surface color and core-temperature control are critical
- High-fat products where rapid post-cook cooling limits fat oxidation and quality loss
For product categories that specifically benefit from steam-injection moisture addition — particularly emulsified sausages and high-moisture whole-muscle hams — the QZX500 steam-injection model remains the preferred technology. Many processors deploy the QLH500 and QZX500 in parallel: the QZX500 for steam-dependent products, the QLH500 for RTE cook-chill and poultry lines. The shared trolley standard means product can move freely between machine types without re-racking.
Chamber Construction & Dimensions
The QLH500 stands 3,480 mm tall — notably taller than the QZX series (2,500 mm) because the refrigeration unit mounts above the cooking chamber. The floor footprint of 1470 × 2600 mm is comparable to the QZX500 (1475 × 2235 mm), making the QLH500 compatible with standard industrial building heights of 4 m or above. Ceiling clearance of at least 3,800 mm is recommended to allow service access to the refrigeration unit.
All internal surfaces are food-grade SUS304 stainless steel, fully welded and polished. The refrigeration coil assembly is stainless-jacketed for corrosion resistance in smoke and condensate environments. Removable smoke-distribution baffles and a sloped chamber floor facilitate efficient wash-down. Door hardware uses cam-action compression latches for reliable sealing across the full operating cycle from smoking temperature down to the chilling endpoint.
Control System & Recipe Programs
The QLH500 uses a Siemens or Mitsubishi PLC with a 7-inch color touch-screen HMI. Up to 99 independent recipe programs are stored on-board, each defining phase-by-phase settings for chamber temperature, air velocity, smoke density, cooling rate target, and HACCP hold conditions. Process parameters are logged at 10-second intervals and archived for 90 days, exportable via USB for food-safety documentation.
Smoke Delivery & Flavor Management in a Forced-Air System
The QLH500 uses an externally mounted smoke generator that pyrolyzes hardwood chips or sawdust at a controlled temperature, producing a cool, phenolic smoke delivered into the chamber through the same air-distribution duct used for heating and cooling. Because the forced-air system moves conditioned air at higher velocity than a conventional passive-draft smokehouse, smoke penetration is highly uniform across both trolley positions, and the smoke phase time required to reach target surface color is predictably shorter than in lower-velocity systems. An optical smoke-density sensor in the exhaust duct feeds back to the PLC to maintain the target concentration set in the active recipe, preventing over-smoking during the early minutes of the smoke phase when the chamber volume fills quickly.
Common wood species used in the QLH500 include beech, alder, cherry, and apple for lighter, more delicate products such as poultry, fish, and soft-casing sausages; hickory and oak for whole-muscle cuts and products targeted at markets with a preference for a stronger smoke character. The wood-fuel choice is a process variable entirely under operator control; the smoke generator is compatible with both standard commercial chips and finer-grade sawdust. For facilities running multiple product types across a single production shift, the recipe system allows a different smoke density target and phase duration to be set for each product program without changing the wood fuel mid-shift.
اکثر پوچھے گئے سوالات
Why does the QLH500 not require steam?
The QLH500 manages moisture through high-velocity forced air rather than steam injection. The forced-air system provides adequate humidity control for the product types the QLH series is optimized for, particularly poultry, RTE cook-chill cuts, and surface-dried sausages. For products requiring active steam-moisture addition, the QZX500 steam-injection model is more appropriate.
What refrigerant does the QLH500 use?
Standard configuration uses R404A or the lower-GWP R452A. The refrigerant specification is confirmed at order stage based on the buyer’s local environmental regulations and the availability of local refrigeration service technicians.
What ceiling height is required for the QLH500?
The QLH500 stands 3,480 mm tall. A minimum ceiling clearance of 3,800 mm is recommended for service access to the refrigeration unit. Verify facility ceiling height before specifying the QLH series.
Can the QLH500 be configured with a pass-through door?
A double-door pass-through option is available for facilities maintaining physical separation between raw and cooked product areas. Specify at the inquiry stage.
QLH500 pre-shipment testing – Hebei Province factory
مینوفیکچرر کے بارے میں
Our company was established in 1999 with a singular focus: reliable, food-safe meat-processing equipment for demanding commercial environments. Today our 5,000 m² Hebei facility manufactures smokehouse systems, vacuum tumblers, brine injectors, sausage filling lines, and clipping machines shipped to buyers in North America, Europe, Southeast Asia, and the Middle East. A dedicated after-sales department provides remote diagnostics, spare-parts dispatch, and on-site commissioning support. Contact us at [email protected].
Shipping & After-Sales
Pre-shipment quality control follows an 8-hour functional test protocol that verifies temperature control accuracy, smoke-density delivery, steam pressure response (QZX models), and cooling performance (QLH models). Results are documented and dispatched with the shipment. Lead time: 30–45 working days. Default incoterm: FOB Tianjin. Warranty period: 12 months from delivery date on all non-consumable parts.
- 8-hour pre-shipment QC with written inspection report
- Temperature, smoke, and pressure performance verified
- 30–45 working-day production lead time
- FOB Tianjin standard; other incoterms on request
- 12-month warranty from delivery date
آرڈر اور لاجسٹکس
Production lead time is 30–45 working days. All units undergo an 8-hour operational test before shipment, with records provided for buyer QC files. Standard incoterm: FOB Tianjin; CIF and EXW available. Terms: 30% T/T deposit, 70% T/T before loading; L/C at sight accepted. Bulk orders of 5+ units qualify for priority scheduling.
Request Technical & Commercial Details
Our engineers can provide datasheet, AutoCAD layout, and FOB price within 24 hours of inquiry.
متعلقہ مصنوعات اور صفحات